Press Die Manufacturing: EDM and Grinding in the Toolroom
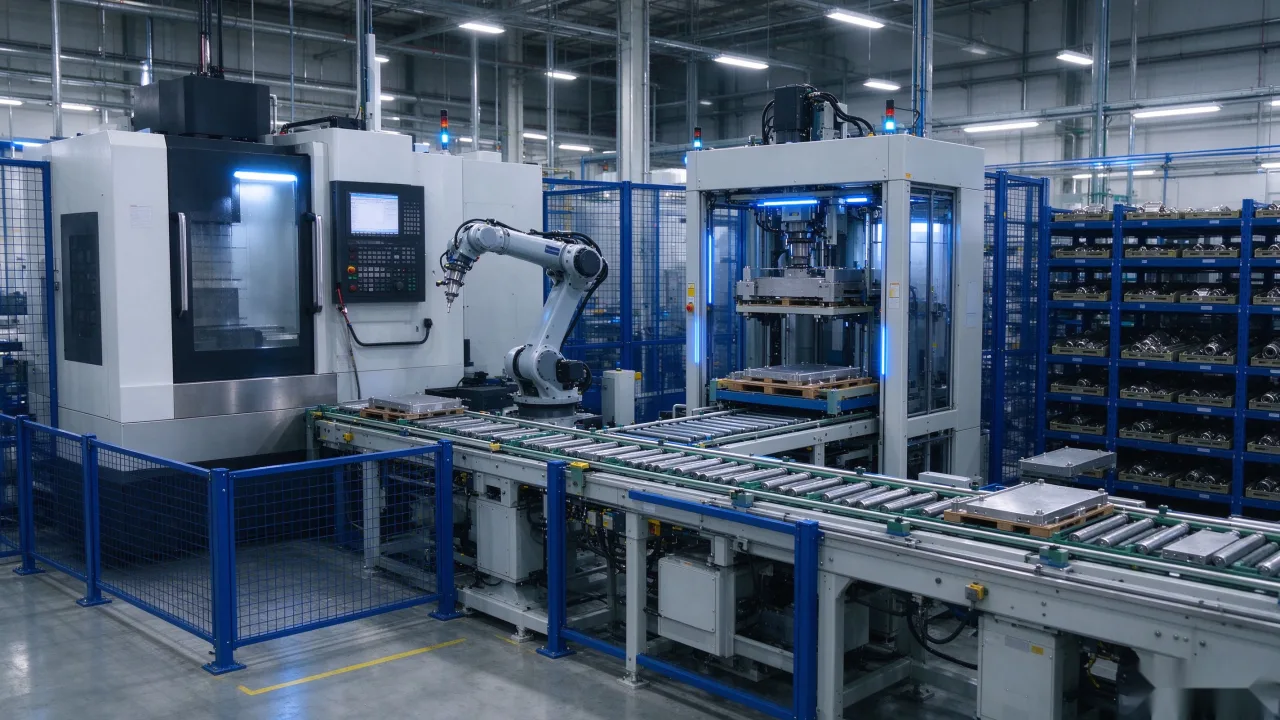
A complete press die toolroom around the machining center: CNC EDM for cavities and details, surface grinders for plates and inserts, and how they sequence.
A machining center shapes the die block, but a finished press die is a team effort. Hardened details, sharp internal corners and mirror flats belong to other machines. A balanced toolroom pairs the VMC or gantry with EDM and precision grinding, and the sequence between them decides both quality and lead time.
Where EDM Takes Over
- Deep ribs and sharp internal corners end-mills cannot reach.
- Hardened D2 and carbide details beyond milling economics.
- Fine lettering, ribs and texture details cut with graphite or copper electrodes.
Our CNC and ZNC EDM series cover oil tanks from 1100 by 710 mm up to 1650 by 1100 mm, with travels from 450 to 700 mm on X, sized for cavity blocks and standard die details. Electrodes for those jobs come from small VMCs or engraving machines overnight.
Where Grinding Finishes the Job
Die plates, strips and inserts need flat, parallel reference faces before anything else fits. Our hydraulic surface grinders, from 460 by 150 mm tables up to large 600 by 300 mm machines, hold those faces so assembly starts square. Ground datum faces also make wire EDM starts predictable.
The practical order: mill and drill soft, heat treat, grind datums, EDM the details, grind finished inserts, assemble. Shops that sequence this way ship dies with fewer fitting hours.
We supply the machines for every step of that chain and help plan the toolroom layout around your die sizes.
Talk to VITOP Machinery
Questions about this topic or your upcoming project? Email vitopmachinery@163.com or message us on WhatsApp: +86 183 1908 0212. Browse all machines at www.vitopmachinery.com. We reply within one business day.