Thin-Wall Machining: Stopping Chatter in Aluminium
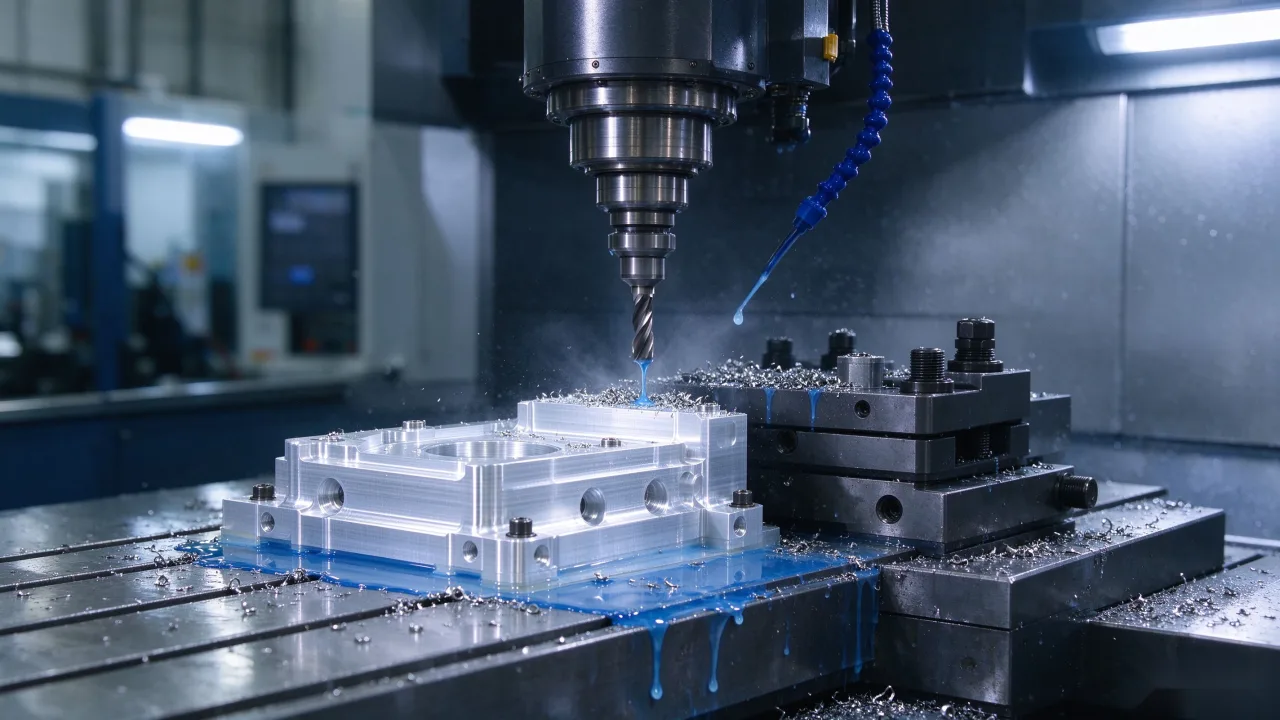
How to machine thin aluminium walls without chatter: fixturing, tool paths, speeds and damping tricks that keep walls straight and on thickness.
Thin-wall aluminium parts look simple and machine hard. The wall you are cutting is the same wall absorbing the cut, so every parameter choice shows up as chatter, taper or waviness. Success is mostly about not exciting the part.
What Actually Works
- High radial engagement with low axial depth keeps forces low and stable.
- Trochoidal paths spread heat and avoid corner overload.
- Sharp, polished, high-helix cutters shear instead of pushing.
- Sacrificial backers and vacuum fixtures support the wall behind the cut.
- Leave the finishing wall for a light final pass after roughing relaxes.
Machine choice helps: fast spindles allow small depths at high speed, and stiff, well-damped structures stop resonance transferring. But fixturing decides most of the outcome. A part held like a drumhead will chatter on the best machine in the world.
Machine choice helps too: fast spindles allow small depths at high speed, and stiff, well-damped structures stop resonance transferring. Our CM and GV series engraving and milling machines pair high spindle speeds with compact, rigid frames, which is why electrode and thin-wall work concentrates on them.
Share your wall thickness and geometry, and we will suggest a strategy with proven parameters for your alloy.
Talk to VITOP Machinery
Questions about this topic or your upcoming project? Email vitopmachinery@163.com or message us on WhatsApp: +86 183 1908 0212. Browse all machines at www.vitopmachinery.com. We reply within one business day.