BF Two-Speed Gearbox for Gantry Machining Center Spindles
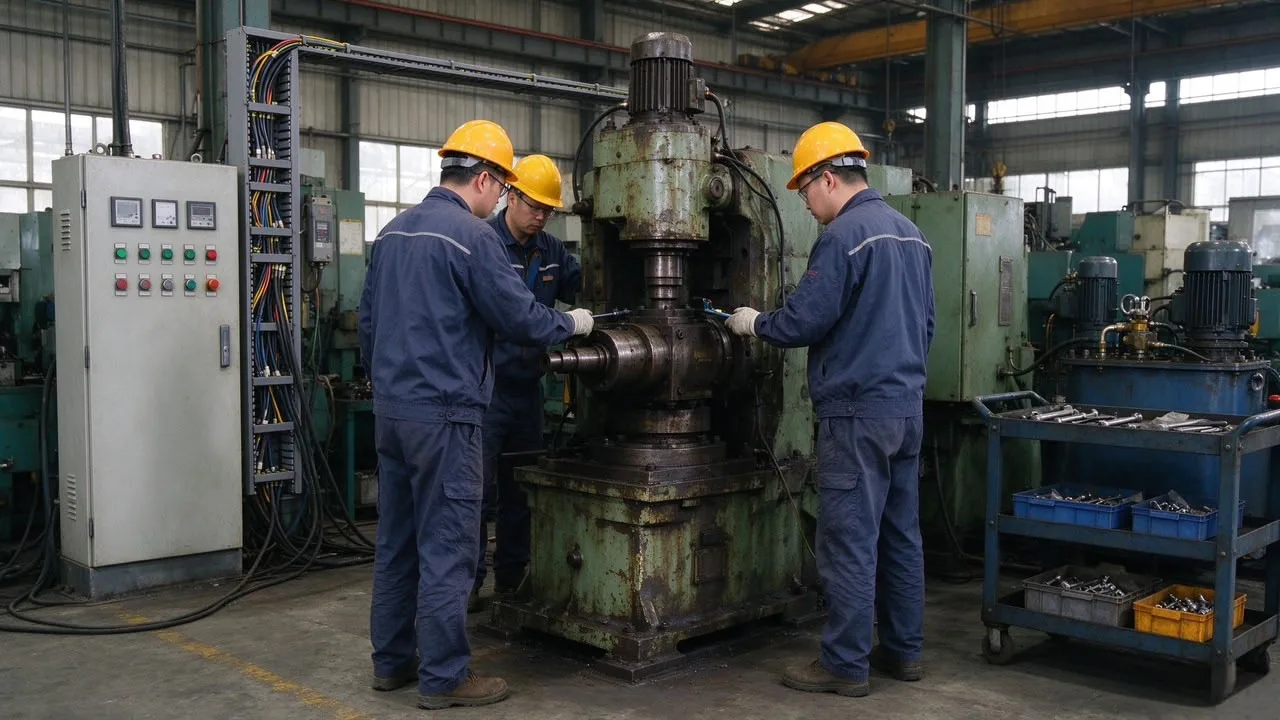
BF series two-speed gearbox for gantry machining center spindle drives, amplifying torque at low spindle speed for heavy roughing of castings and structural parts.
A gantry machining centre lives or dies by its cutting force. You can have the widest table and the heaviest column in the industry, but if the spindle runs out of torque halfway into a roughing pass on a large casting, the machine is only half a machine. The BF two-speed gearbox is VITOP's optional equipment for gantry machining center spindle drives, and its job is simple to state: amplify torque at low spindle speed.
What a Two-Speed Gearbox Actually Does
An electric motor delivers its power across a speed range, but torque at low rpm is limited unless something multiplies it. A two-speed gearbox sits between the motor and the spindle and offers two ratios. In low gear, the spindle turns slowly and the motor's torque is multiplied, which is what a heavy roughing cut needs: big depth of cut, big width of cut, low surface speed. In high gear, the spindle runs faster for finishing, facing and lighter work where surface speed matters more than raw torque.
One machine, two working characters. Without the gearbox, a spindle sized for heavy cutting would be sluggish at finishing speeds, and a spindle sized for finishing would stall in a heavy cut.
When You Need It
Look honestly at your part mix. The gearbox earns its place when your work looks like this:
- Large castings with thick machining allowances
- Structural parts, welded fabrications and machine bases
- Hard or tough materials where cutters run slowly by necessity
- Mould work with heavy pocketing before finishing passes
If instead you mostly machine aluminium panels, plastics or thin finishing passes at higher spindle speeds, the gearbox adds cost and complexity without much return. Buy it for the roughing hours you actually run, not for the worst case you imagine once a year.
How It Changes Daily Operation
In practice, the gearbox changes how your CAM programmer works. Low gear supports aggressive insert milling at low rpm with the full motor power behind the cut, so cycle time on roughing drops noticeably. High gear covers the finishing passes without a tool or spindle change. The gear shift is programmed into the part programme like any other spindle command, so the transition happens automatically between operations.
There is also a machine-health angle. When the spindle has torque in reserve, cutters last longer because loads stay stable instead of peaking and stalling. Stable loads also mean less stress passed into the column and the workpiece setup, which shows up as better flatness on large parts.
Specifying It With Your Machine
The BF gearbox is specified as optional equipment on VITOP gantry machining centers, matched to the spindle drive of the machine. When you request a quotation, describe your cutting honestly: material, allowance depth, cutter diameters and the share of roughing versus finishing hours. That is what determines whether the gearbox is worth specifying and which configuration suits your duty cycle.
Two practical questions to settle before ordering:
- What is the largest cutter and depth of cut you expect to run, and at what spindle speed?
- How much of your weekly spindle time is heavy roughing versus finishing?
If the answers point to long roughing hours on heavy material, the BF gearbox will pay for itself in reduced cycle time and longer tool life. Send your typical part drawings to us and we will help you match the drive configuration to the work.
Talk to VITOP Machinery
Planning a machine purchase or need help matching a model to your parts? Send your drawings or questions to vitopmachinery@163.com, or message us directly on WhatsApp: +86 183 1908 0212. You can also browse all machines at www.vitopmachinery.com. We reply within one business day.
Need a CNC Machine for Your Project?
Tell us what you need to machine — our engineers will recommend the right model and send a quotation within 24 hours.