High-Efficiency EDM Machine for Large Mould Work
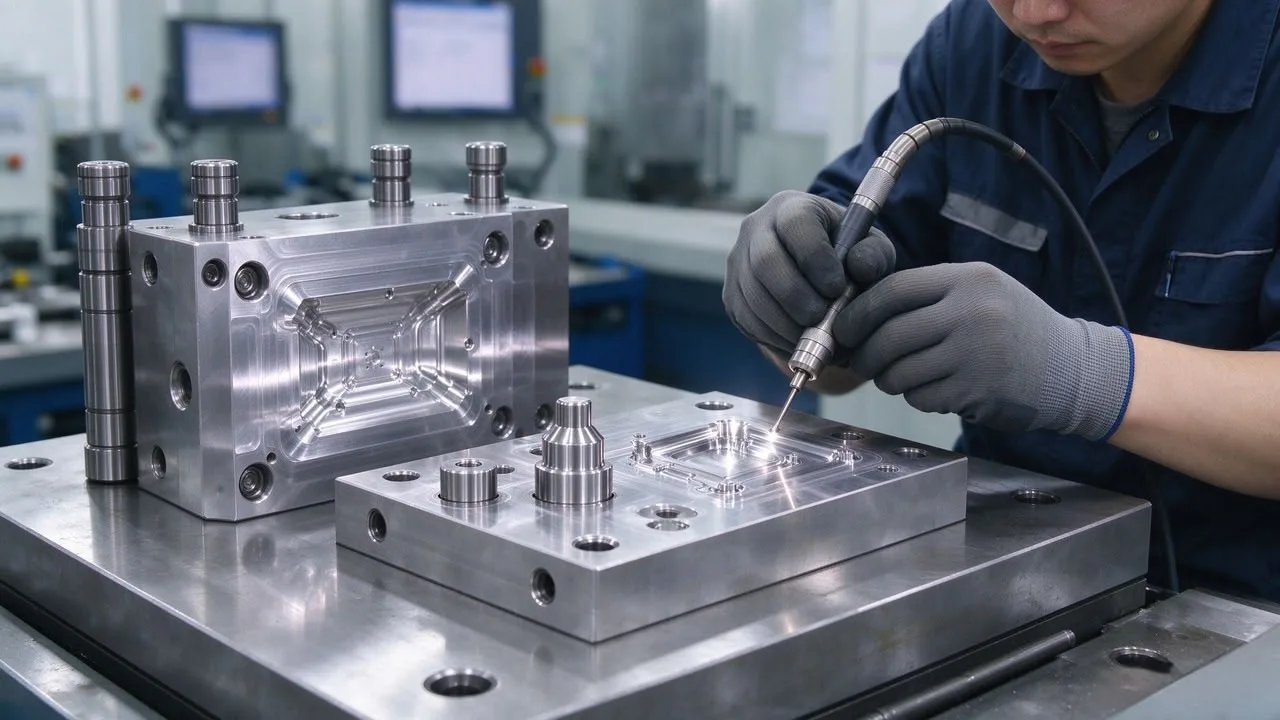
High-efficiency EDM series from CNC430N to CNC1880NN with work tanks up to 3500 x 1800 x 630 mm, workpiece loads to 6500 kg plus electrode loads to 450 kg.
Standard die sinking machines cover most cavity work. Then a job comes along that does not fit: a large automotive mould, an appliance panel tool, a bumper mould half, a set of oversized insert blocks. That is the territory of the VITOP high-efficiency EDM series, six models from CNC430N up to CNC1880NN, built for stable discharge machining on big workpieces.
An Envelope That Grows With Your Moulds
The smallest model in the series takes a work tank of 1130 x 710 x 450 mm. From there the range steps up through 1370 x 810 x 450 mm and beyond, to a maximum of 3500 x 1800 x 630 mm on the largest machine. Working travels scale the same way, from 450 x 330 x 300 mm on the compact model to 1200 x 800 x 600 mm at the top of the range.
| Parameter | Series range |
|---|---|
| Work tank (L x W x H) | 1130 x 710 x 450 up to 3500 x 1800 x 630 mm |
| Table size | 700 x 400 up to 2000 x 1000 mm |
| Working travel X x Y x Z | 450 x 330 x 300 up to 1200 x 800 x 600 mm |
| Spindle head to table (high/low) | 310-610 up to 630-1230 mm |
| Max. electrode weight | 120 to 450 kg |
| Max. workpiece load | 1500 to 6500 kg |
| Whole machine weight | 1800 to 15000 kg |
Why Load Capacity Matters in EDM
On small EDM work, load ratings are a formality. On large mould work they decide what you can burn in one setup. This series carries workpieces from 1500 kg on the smaller machines to 6500 kg on the largest, and accepts electrodes from 120 up to 450 kg. That combination means a heavy cavity block can stay clamped on the table while several electrodes, rougher and finisher, are changed and burned in sequence. Every extra setup you avoid is a re-alignment you do not have to fight.
The spindle head position range, up to 630 to 1230 mm from table to head on the large models, gives clearance for tall cores, deep cavity bases and substantial electrode holders.
Where This Series Earns Its Keep
- Automotive bumper, dashboard and panel moulds
- Large appliance and container mould cavities
- Oversized insert and slide details in hardened steel
- Deep rib and groove details where cutters cannot reach
Plan the Floor Before the Machine Arrives
The largest model weighs up to 15000 kg before you add a workpiece. Compare that with the 1800 kg of the smallest: the series spans a wide range of installation requirements. Check floor loading, crane access for unloading, and the power supply at the planned position. A machine this size is not moved again easily, so walk the route from the door to the foundation first and measure door widths and floor openings with a tape, not by eye.
Electrode and flushing practice deserve attention on machines of this size. Large graphite or copper electrodes burn for hours, so plan how each one will be clamped and aligned before the block goes on the table. Good flushing is equally important: in a deep cavity the debris has a long way to travel, and a burn that looks fine on the surface can be re-cutting debris at the bottom. Build flushing holes into the electrode design where you can, and discuss the deep details with us early rather than after the first burn.
Choosing Between the EDM Ranges
If your largest cavity block fits under 700 mm of X travel and under 2000 kg, the standard CNC/ZNC series is usually the more economical choice. Once your work regularly exceeds those figures, or your electrodes push past 200 kg, the high-efficiency series is the right tool. Send us your largest part drawing and electrode plan, and we will suggest which model covers it with sensible margin.
Talk to VITOP Machinery
Planning a machine purchase or need help matching a model to your parts? Send your drawings or questions to vitopmachinery@163.com, or message us directly on WhatsApp: +86 183 1908 0212. You can also browse all machines at www.vitopmachinery.com. We reply within one business day.
Need a CNC Machine for Your Project?
Tell us what you need to machine — our engineers will recommend the right model and send a quotation within 24 hours.